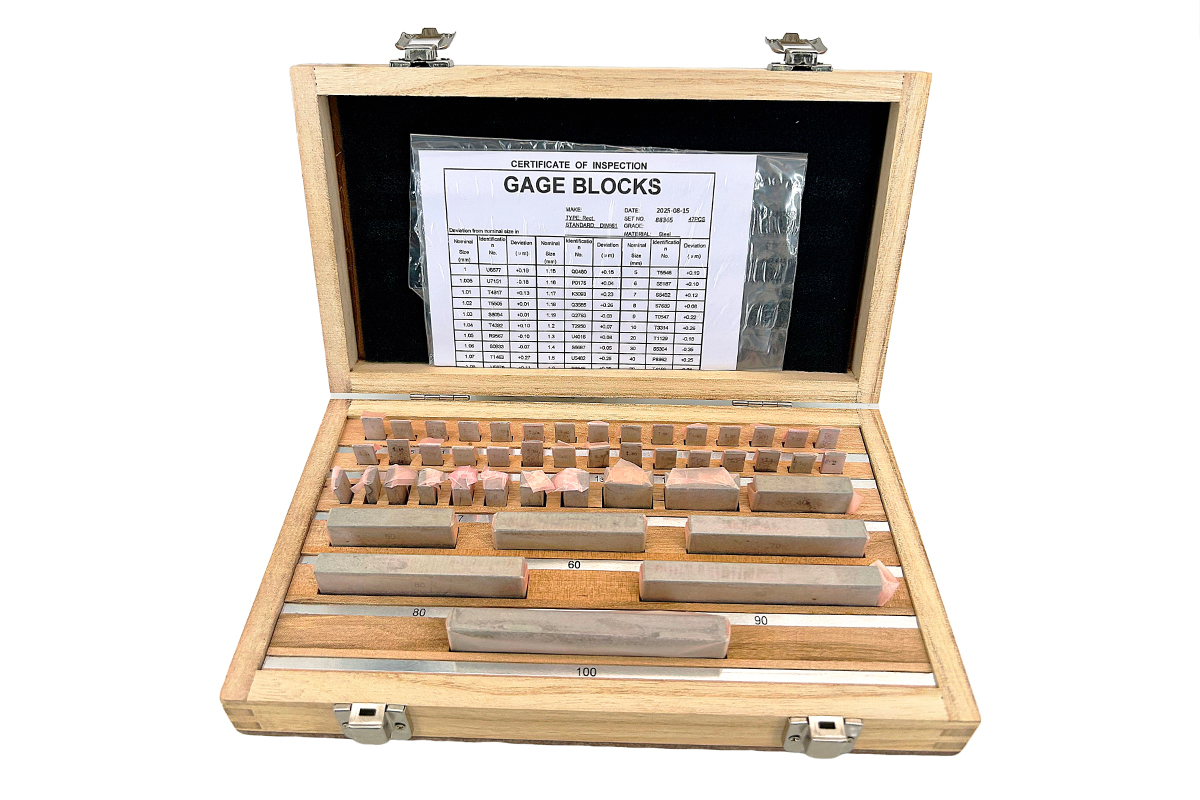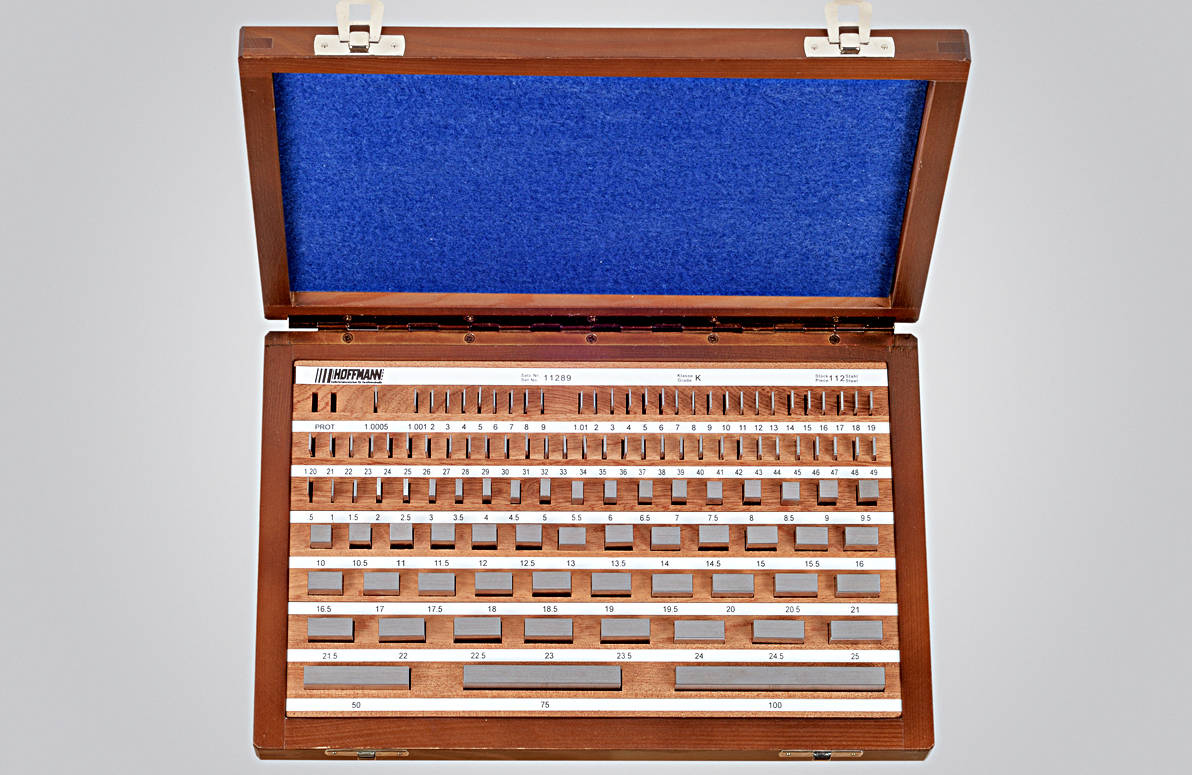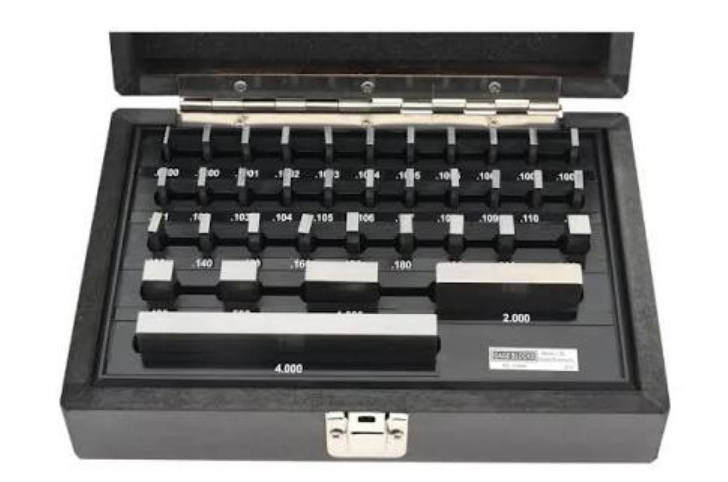
Choosing between Grade 0, Grade 1, and Grade 2 gauge blocks should start with the measurement task—not with the assumption that the highest grade is automatically the right purchase.
As a practical selection framework:
- Grade 0 gauge blocks are commonly chosen for higher-accuracy inspection, calibration, and reference work.
- Grade 1 gauge blocks are well suited to many quality-control rooms and general precision inspection tasks.
- Grade 2 gauge blocks are commonly used for workshop, production, setup, and general-purpose dimensional checking.
- Calibration Grade K sits above this simple production hierarchy and is intended for higher-level calibration applications.
ISO 3650 specifies calibration Grade K and Grades 0, 1, and 2, with different limit deviations and tolerances for different measuring purposes. Those tolerances vary with nominal block length, so a grade should not be treated as one universal ±µm value.
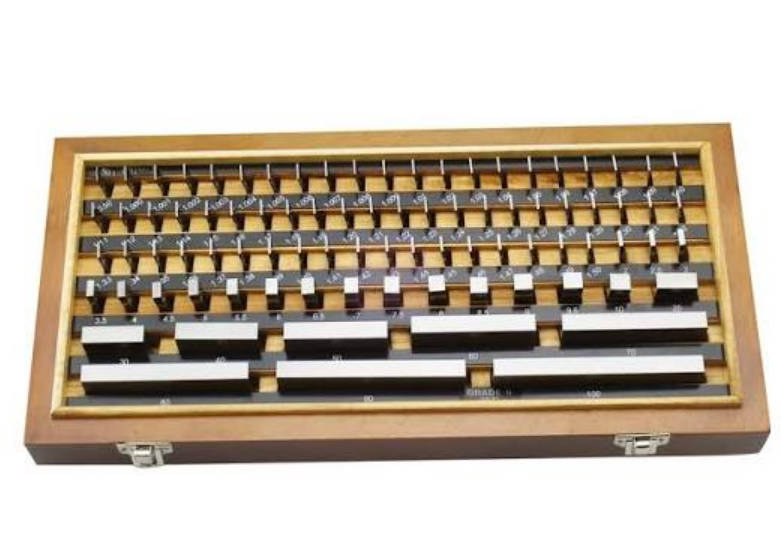
MISHUTE currently provides precision gauge blocks in Grade 0, Grade 1, and Grade 2, with Grade K available for calibration-oriented requirements. (mishute.com)
First Question: Where Will the Gauge Blocks Sit in Your Measurement Chain?
Instead of beginning with a specification table, picture your measurement system as a hierarchy.
At the top are reference standards.
Below them are working standards used to verify inspection equipment.
Further down are shop-floor tools used to set or check production measurements.
The closer a gauge block sits to the top of that chain, the stronger the case for tighter dimensional control and more detailed calibration data.
| Measurement Role | Typical Gauge Block Choice | Main Priority |
| High-level reference or calibration work | Grade K or Grade 0 depending on system requirements | Lowest practical uncertainty |
| Precision calibration or high-accuracy inspection | Grade 0 | Tighter dimensional control |
| Quality-control room | Grade 1 | Accuracy balanced with practical use |
| Machine shop or production inspection | Grade 2 | Robust, economical working standard |
| High-risk measurement with customer-defined requirements | Determined from uncertainty analysis | Compliance with required measurement capability |
The correct gauge block grade is the lowest grade that still supports the uncertainty and tolerance requirements of your measurement process.
Buying a tighter grade than necessary can increase cost without improving the final measurement if the rest of the system cannot use that additional accuracy.
Scenario 1: You Are Building a Calibration or Reference Set
Suppose the blocks will be used to:
- Calibrate precision comparators
- Verify master instruments
- Support internal metrology
- Provide reference values for other working standards
- Maintain dimensional traceability
This is a very different job from checking a micrometer beside a CNC machine.
Consider Grade 0
Grade 0 is commonly used where tighter dimensional control is required and the blocks form part of a high-accuracy inspection or calibration system.
Potential users include:
- Metrology rooms
- Calibration departments
- Precision laboratories
- Toolrooms maintaining reference standards
A Grade 0 set makes the most sense when the surrounding measurement system can actually support it.
That means considering:
- Calibration uncertainty
- Temperature control
- Wringing technique
- Block cleanliness
- Comparator capability
- Calibration history
A Grade 0 block used on a dirty shop-floor bench does not automatically produce a Grade 0 measurement.
When Grade K Enters the Discussion
ISO 3650 also defines calibration Grade K separately from Grades 0, 1, and 2.
Grade K is relevant when the blocks themselves are being used as calibration standards and detailed calibrated values are important.
NIST distinguishes between simply certifying that a gauge block falls within a tolerance grade and calibrating the individual block so that its measured length is actually reported.
That distinction matters.
If your process uses the actual calibrated correction of each block, certificate quality may matter as much as the nominal grade printed on the set.
Scenario 2: Your Gauge Blocks Live in the QC Room
Now consider a manufacturing company with a dedicated quality-control room.
The blocks are routinely used to:
- Check micrometers
- Verify calipers
- Set bore gauges
- Set dial comparators
- Check height measuring equipment
- Support incoming and final inspection
The environment is controlled reasonably well, but the blocks are working tools rather than top-level laboratory references.
Grade 1 Is Often the Practical Middle Ground
Grade 1 gauge blocks can make sense here because they balance dimensional capability with routine industrial use.
A QC department usually needs better control than a general machine-shop working set, but it may not gain meaningful value from purchasing Grade 0 for every size.
Grade 1 may therefore suit organizations that need:
- Reliable precision inspection
- Regular instrument verification
- Controlled measurement-room use
- Reasonable procurement cost
- Working standards that are more accurate than general shop-floor blocks
Grade 1 is often a logical working-standard grade when the application requires precision but does not justify the tighter cost and control requirements associated with Grade 0.
The decision should still be based on your tolerance and uncertainty requirements rather than on the department name.
Scenario 3: The Blocks Will Be Used on the Production Floor
Now imagine gauge blocks kept near machining equipment.
Operators use them to:
- Check measuring tools
- Set fixtures
- Verify machine setups
- Compare manufactured dimensions
- Perform routine workshop inspection
The environment may involve:
- Temperature variation
- Coolant
- Oil
- Frequent handling
- Higher contamination risk
- Greater chance of wear or accidental damage
Grade 2 Is Often Appropriate
Grade 2 gauge blocks are commonly selected for general workshop and production use.
The logic is straightforward.
If the measurement task does not require laboratory-level uncertainty, spending more on a substantially tighter grade may not improve the production decision.
A Grade 2 set can still be a precision dimensional standard.
The word “Grade 2” should not be interpreted as “low quality.”
It refers to the tolerance classification of the gauge block.
Grade 2 can be the technically correct choice when the block is used as a working standard in normal production inspection.
For these applications, buyers can review gauge block sets for workshop and inspection use rather than automatically specifying the tightest available grade.
Grade 0 vs Grade 1 vs Grade 2 at a Glance
| Selection Factor | Grade 0 | Grade 1 | Grade 2 |
| Relative tolerance control | Tightest of the three | Intermediate | Wider |
| Typical role | Higher-accuracy reference / inspection | QC working standard | Workshop working standard |
| Calibration work | Strong fit | Suitable for many internal checks | More limited |
| Quality-control room | Suitable | Strong fit | Possible depending on tolerance |
| Shop-floor use | Technically possible but may be excessive | Suitable for tighter production work | Strong fit |
| Environmental control expected | Higher | Moderate to high | Normal industrial control |
| Handling discipline | High | High | Still important |
| Purchase cost | Generally higher | Intermediate | Generally lower |
| Best buying logic | Accuracy requirement justifies it | Balanced precision | Practical production use |
This table is a selection guide, not a replacement for the tolerance tables in the applicable gauge block standard.
ISO 3650 defines the actual limit deviations and tolerances by grade and nominal length.
Why the Grade Difference Cannot Be Reduced to One Number
Buyers often search for something like:
Grade 0 tolerance = ?
Grade 1 tolerance = ?
Grade 2 tolerance = ?
The problem is that gauge block tolerances are not represented correctly by one fixed tolerance for every block length.
A 1 mm block and a 500 mm block do not share the same practical tolerance limits.
This is one reason ISO 3650 specifies tolerance limits across the applicable length range rather than assigning a single universal deviation to every block within one grade.
So when requesting a quotation, do not specify only:
Gauge blocks ±0.1 µm
unless that is genuinely your own custom engineering requirement.
A better RFQ specifies:
- Standard
- Grade
- Set composition
- Material
- Calibration requirement
Higher Grade Does Not Automatically Mean Better Measurement
This is probably the most important buying misconception.
Imagine two measurement systems.
System A
- Grade 0 blocks
- Uncontrolled workshop temperature
- Dirty measurement surfaces
- Excessive hand handling
- Uncalibrated comparator
System B
- Grade 1 blocks
- Controlled inspection environment
- Documented calibration
- Proper wringing
- Stable comparator
- Trained operator
System B may provide the more reliable result despite using a nominally lower gauge block grade.
Gauge block accuracy is only one component of the measurement system.
Other error sources include:
- Temperature
- Thermal expansion
- Wringing
- Surface cleanliness
- Comparator repeatability
- Contact deformation
- Operator technique
- Calibration uncertainty
NIST’s gauge block metrology work treats temperature, geometry, deformation, comparison methods, wringing, and calibration uncertainty as integral parts of gauge block measurement—not secondary details.
A tighter gauge block grade cannot compensate for an uncontrolled measurement process.
Work Backward From the Part Tolerance
A better selection method begins with the manufactured component.
Suppose you are measuring a tightly toleranced bore.
Ask:
- What is the part tolerance?
- What measurement uncertainty is acceptable?
- What instrument will perform the measurement?
- What reference will calibrate or set that instrument?
- What uncertainty can the gauge block contribute?
This creates a measurement chain.
The gauge block grade should support that chain without becoming the dominant uncertainty source.
For Relatively Wide Production Tolerances
Grade 2 may provide sufficient capability.
For Precision QC
Grade 1 may offer a better margin.
For High-Accuracy Calibration or Reference Work
Grade 0 or Grade K may become appropriate.
This is much more defensible than selecting Grade 0 simply because the purchasing budget allows it.
Do You Need Grade 0 for Micrometer Calibration?
Not automatically.
The correct answer depends on:
- Micrometer resolution
- Required calibration uncertainty
- Instrument accuracy specification
- Customer requirements
- Calibration method
- Gauge block uncertainty
For ordinary production micrometers, a well-controlled Grade 1 or even appropriately calibrated Grade 2 set may support the required check in some applications.
For higher-accuracy calibration work, Grade 0 may provide a stronger uncertainty margin.
The point is not that one grade is always sufficient.
The point is that the gauge block should be selected relative to the device being calibrated and the uncertainty required.
Should a QC Department Buy Grade 0 “Just to Be Safe”?
Sometimes this is reasonable.
Often it is not necessary.
Purchasing Grade 0 “for safety” creates additional questions:
- Will the blocks receive appropriate calibration?
- Is the room controlled well enough?
- Will operators use the calibrated corrections?
- Is the measurement equipment capable of taking advantage of the tighter grade?
- Will the blocks be handled like reference standards?
- Does the customer actually require it?
If the answer to most of these questions is no, Grade 1 may produce essentially the same practical inspection outcome at a lower acquisition cost.
A higher-grade product only creates value when the measurement system can preserve and use that additional capability.
Can Grade 2 Be Used to Check Precision Instruments?
Potentially, but the required uncertainty must be evaluated.
This is where simply labeling Grade 2 as “workshop grade” can be misleading.
A properly calibrated Grade 2 block has a known dimensional condition.
Whether it is suitable depends on the required instrument calibration.
For some general-purpose measuring tools, it may be adequate.
For tighter metrology work, it may not provide enough margin.
The key distinction is:
Grade defines allowable characteristics of the block; your measurement uncertainty determines whether those characteristics are adequate for the task.
Material and Grade Are Two Separate Decisions
Do not confuse gauge block material with gauge block grade.
MISHUTE currently offers gauge blocks in:
- Zirconia ceramic
- Tungsten carbide
- Hardened steel
with Grade 0, Grade 1, and Grade 2 options, as well as Grade K for calibration-oriented requirements. (mishute.com)
This means you could specify, for example:
- Grade 0 ceramic gauge blocks
- Grade 1 steel gauge blocks
- Grade 2 steel gauge blocks
- Grade 0 tungsten carbide gauge blocks
Material affects characteristics such as:
- Wear resistance
- Corrosion behavior
- Thermal behavior
- Maintenance
- Handling
- Purchase cost
Grade controls the metrological tolerance classification.
Choose the grade according to measurement accuracy; choose the material according to the operating environment.
Buyers can compare available precision gauge block grades and materials as two separate specification decisions.
A Smarter Strategy: Do Not Use the Same Grade Everywhere
A factory does not necessarily need one universal grade.
Consider a three-level system.
Reference Set
Grade 0 or another appropriate higher-level standard.
Kept in a controlled environment and used primarily to verify working standards.
QC Working Set
Grade 1.
Used by the inspection department for routine calibration and dimensional setup.
Workshop Set
Grade 2.
Used by machinists and production inspectors for daily checking.
This creates a rational hierarchy.
The more valuable and accurate reference blocks are protected from unnecessary production wear, while lower-level working sets handle daily use.
Over time, this can be more economical than buying Grade 0 sets for every department.
What About Grade K?
Although the article focuses on Grade 0 vs Grade 1 vs Grade 2, buyers should understand why Grade K exists.
ISO 3650 identifies Grade K as a calibration grade separately from Grades 0, 1, and 2.
Grade K should therefore not simply be described as “Grade 0 but better.”
Its role is more closely tied to calibration use.
For organizations maintaining high-level reference standards, the purchasing discussion should include:
- Individual calibrated values
- Measurement uncertainty
- Calibration method
- Traceability
- Long-term stability
- Calibration certificate requirements
MISHUTE lists Grade K customization alongside its Grade 0, Grade 1, and Grade 2 gauge block sets.
Calibration Certificate Matters More as the Grade Gets Tighter
If Grade 2 blocks are used for routine shop-floor checking, a factory inspection report may support many purchasing situations depending on the quality system.
When Grade 0 or Grade K blocks are purchased for reference use, documentation becomes increasingly important.
Buyers may need:
- Individual measured deviation
- Calibration uncertainty
- Traceability information
- Calibration date
- Laboratory identification
- Certificate number
- Applicable standard
- Grade statement
- Third-party calibration where required
The tighter the intended measurement responsibility, the less sensible it becomes to evaluate the block only by the grade printed on its case.
A Practical RFQ Example
Instead of writing:
Please quote a high-accuracy gauge block set.
send a specification such as:
Metric gauge block set, ISO 3650 Grade 1, hardened steel, intended for QC-room calibration of production measuring instruments. Please confirm set composition and available inspection/calibration documentation.
For a higher-level requirement:
Metric gauge block set, ISO 3650 Grade 0, zirconia ceramic, intended for precision reference and calibration work. Please provide available calibration documentation and third-party certification options.
For general production:
Metric Grade 2 gauge block set for workshop measurement and measuring-tool verification.
These descriptions immediately give the supplier more useful purchasing information.
Five Costly Grade-Selection Mistakes
Mistake 1: Buying Grade 0 Because It Sounds More Professional
If the measurement system cannot use the additional accuracy, you are paying for unused capability.
Mistake 2: Using Grade 2 Everywhere Because It Is Cheaper
A reference or calibration laboratory may require tighter control than Grade 2 can provide for the intended uncertainty.
Mistake 3: Selecting Grade Before Defining the Measurement
You cannot make a rational grade choice without understanding the tolerance, instrument, and uncertainty requirement.
Mistake 4: Assuming Grade Equals Calibration
A tolerance grade and an actual calibrated length value are different concepts.
NIST specifically distinguishes industrial tolerance-grade certification from calibration that reports measured block length. (NIST)
Mistake 5: Forgetting Wear and Environment
A higher grade that becomes damaged, corroded, contaminated, or badly worn is not a better working standard.
Quick Buyer Decision Guide
Use these questions before placing the order.
Are the blocks top-level calibration or reference standards?
Evaluate Grade K or Grade 0, depending on the measurement system.
Will they be used for high-accuracy calibration or precision comparison?
Start with Grade 0.
Will they be used primarily in a controlled QC room?
Grade 1 is often a practical starting point.
Will machinists use them for routine workshop measurement?
Grade 2 is commonly appropriate.
Does the customer specify a particular grade?
Follow the contractual specification.
Are you still unsure?
Provide the part tolerance, measuring instrument, intended use, and calibration requirement to the supplier instead of guessing a grade.
Frequently Asked Questions
What is the difference between Grade 0, Grade 1, and Grade 2 gauge blocks?
Grade 0 has tighter dimensional tolerance requirements than Grade 1, while Grade 1 is tighter than Grade 2. The actual permitted deviations depend on nominal block length and the applicable standard.
Which gauge block grade is most accurate?
Among Grade 0, Grade 1, and Grade 2, Grade 0 has the tighter tolerance classification. ISO 3650 also defines a separate calibration Grade K for calibration-oriented applications.
What are Grade 0 gauge blocks used for?
Grade 0 gauge blocks are commonly used for high-accuracy inspection, calibration, toolroom reference, and metrology applications where tighter block tolerances are useful.
What are Grade 1 gauge blocks used for?
Grade 1 gauge blocks are commonly suited to quality-control rooms, precision inspection, instrument verification, and working-standard applications.
What are Grade 2 gauge blocks used for?
Grade 2 gauge blocks are commonly used for general workshop measurement, machine setup, production inspection, and routine checking of measuring tools.
Is Grade 0 always better than Grade 1?
Grade 0 has tighter tolerance requirements, but it is not automatically the better purchase. If the measurement process does not require or support the additional accuracy, Grade 1 may be more economical and entirely adequate.
Can Grade 2 gauge blocks be used to calibrate micrometers?
They may be suitable for some general-purpose calibration or verification tasks, depending on the required measurement uncertainty. The complete calibration system must be evaluated rather than selecting a grade by name alone.
What is Grade K in gauge blocks?
Grade K is a calibration grade defined by ISO 3650. It is intended for calibration-oriented use and should not simply be treated as another production working grade.
Does gauge block material affect the grade?
Material and grade are separate specifications. Steel, ceramic, or tungsten carbide gauge blocks can be manufactured to different grades when the manufacturer supports those combinations.
Should I buy Grade 0 gauge blocks for a CNC workshop?
Usually only if the measurement requirement justifies them. Grade 2 is commonly more practical for routine workshop use, while Grade 1 may suit tighter production or QC applications.
Which gauge block grade should a quality-control room use?
Grade 1 is often a practical starting point for QC-room working standards. Grade 0 may be appropriate when the room performs higher-accuracy calibration or reference measurements.
Conclusion: Choose the Grade by Measurement Responsibility
Gauge block grades should not be treated as a simple good-better-best product ladder.
They represent different levels of dimensional control for different measurement responsibilities.
Use Grade 0 when higher-accuracy reference or calibration work justifies tighter tolerances. Consider Grade 1 for precision QC and working-standard applications. Use Grade 2 where practical workshop and production measurement is the priority.
For higher-level calibration systems, also consider whether Grade K and individual calibrated values are more appropriate.
The purchasing decision should ultimately combine:
- Required measurement uncertainty
- Part tolerance
- Instrument capability
- Measurement environment
- Frequency of use
- Gauge block material
- Calibration documentation
- Budget
MISHUTE provides Grade 0, Grade 1 and Grade 2 gauge blocks in multiple material options, with calibration-oriented Grade K requirements also available for suitable applications.
For organizations building a complete dimensional-control system, MISHUTE can also serve as a precision gauge manufacturer for gauge block and related inspection requirements.