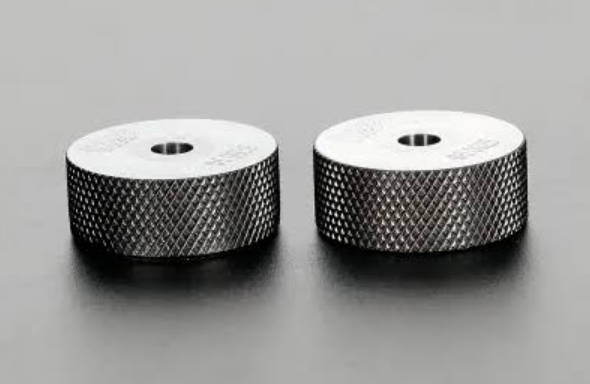
When purchasing a precision ring gauge, the nominal diameter marked on the gauge is only the starting point.
For production GO/NO-GO inspection, the main concern is whether the ring has been manufactured and verified within the specified gauge limits. For a master or setting ring, the actual calibrated internal diameter becomes much more important because another measuring instrument may be set from that value.
A useful ring gauge calibration certificate should identify the exact gauge, report its calibrated size or deviation where required, state the measurement uncertainty, and provide enough information to support traceability of the measurement result.
The required level of calibration therefore depends heavily on what the ring gauge does in your measurement system.
A production ring used to accept shafts and a master ring used to set a bore gauge may look similar, but the consequences of calibration error are very different.
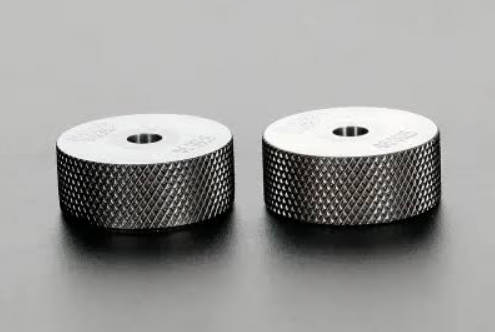
MISHUTE supplies precision ring gauges for production inspection and master or setting applications, with several tolerance classes, material options, factory inspection reports, and third-party certification options available.
Two Ring Gauges Can Have the Same Nominal Size but Very Different Calibration Needs
Consider two gauges, both marked:
Ø25.000 mm
The first is a GO ring used on a production line.
The second is a master setting ring used to zero a precision bore gauge.
They share the same nominal diameter, but they do not perform the same job.
Production GO Ring
The production operator mainly needs to know:
Does the external part pass the specified size limit?
The gauge is a physical acceptance limit.
Its calibration or inspection documentation should confirm that the gauge itself remains within the required manufacturing limits.
Master or Setting Ring
The metrology technician asks a different question:
What is the actual calibrated internal diameter that should be assigned to this ring?
If the ring’s calibrated value differs slightly from nominal, that correction may affect how the bore-measuring instrument is set.
For a setting ring, “25.000 mm nominal” and “25.000 mm calibrated value” should not automatically be treated as the same statement.
That distinction determines what buyers should request on the certificate.
Start by Identifying the Function of the Ring
Before discussing accuracy, identify which type of ring you are buying.
| Ring Gauge Function | Main Measurement Purpose | Calibration Priority |
| GO ring gauge | Accept maximum permitted external size condition | Verify gauge limit |
| NO-GO ring gauge | Reject parts crossing the opposing size limit | Verify gauge limit |
| Master ring gauge | Provide a dimensional reference | Accurate assigned bore value |
| Setting ring gauge | Set or zero an internal measuring instrument | Accurate assigned bore value and uncertainty |
| Reference ring | Monitor or compare measuring equipment | Stable calibrated value |
| Custom ring gauge | Application-specific inspection | Depends on function |
This distinction should appear in the RFQ.
Do not simply order:
Ø25 mm ring gauge.
A more useful specification is:
Ø25 mm master setting ring for setting a bore gauge.
or:
Ø25 mm GO plain ring gauge for production shaft inspection.
MISHUTE’s ring gauge solutions cover both production inspection rings and master/setting applications.
What Does “Ring Gauge Accuracy” Actually Mean?
Buyers often ask:
What accuracy is this ring gauge?
That question can refer to several different characteristics.
Bore Diameter
This is the most obvious value.
The internal diameter must meet the required specification or have an assigned calibrated value appropriate to the ring’s intended use.
Roundness
A bore can have the correct average diameter and still contain geometric variation.
For example, a ring may be slightly oval rather than perfectly circular.
For a precision master, this can matter because a bore gauge may contact the ring at different angular positions.
Cylindrical Form
The internal surface should also behave consistently along the usable gauging length.
Possible errors include:
- Taper
- Barrel shape
- Bell-mouth
- Local wear
A diameter measured at one cross-section does not necessarily describe the complete bore.
Surface Condition
The measuring surface affects:
- Contact behavior
- Repeatability
- Wear
- Stability
- Risk of damaging the instrument or workpiece
Burrs, corrosion, scratches, and contamination can all interfere with precision use.
Measurement Uncertainty
The calibration result itself also carries uncertainty.
This determines how confidently the reported internal diameter can be used as a reference.
For a master ring, useful calibration is not simply about producing a small dimensional number; it is about understanding the calibrated value together with its uncertainty and bore condition.
The Certificate Should Identify the Exact Ring
Imagine your quality department owns five rings:
- Ø10 mm
- Ø20 mm
- Ø25 mm
- Ø30 mm
- Ø50 mm
Three are later replaced.
Two are recalibrated.
One remains in the original case.
Without strong identification, it becomes surprisingly easy to attach the wrong document to the wrong gauge.
A ring gauge certificate should therefore provide sufficient identification, such as:
- Manufacturer
- Product description
- Nominal size
- Gauge type
- Serial number or unique ID
- Customer gauge number where applicable
- Material
- Calibration date
- Certificate number
For matched GO/NO-GO sets, the documentation should make clear which result belongs to which ring.
A certificate that cannot be reliably linked to the physical gauge creates a traceability problem even if the measurement itself was technically excellent.
Check the Actual Measured Diameter
For master and setting rings, buyers should pay particular attention to the assigned internal diameter.
A simplified calibration table might look like this:
| Gauge | Nominal Size | Measured Size | Deviation |
| Setting Ring A | 20.000 mm | 20.0004 mm | +0.0004 mm |
| Setting Ring B | 30.000 mm | 29.9997 mm | -0.0003 mm |
These values are purely illustrative.
They are not specifications for MISHUTE products.
The point is that the measured size may differ slightly from nominal while the ring remains suitable for its intended specification.
When setting a high-resolution comparator or bore gauge, the user may need to set the instrument according to the calibrated value rather than blindly entering the nominal marking.
This is one reason buyers looking for calibrated ring gauges should define whether individual measurement results are required in the purchasing specification.
Nominal Size, Tolerance and Calibrated Value Are Different Things
These three concepts should not be mixed together.
Nominal Size
The intended basic diameter.
Example:
25.000 mm
Gauge Tolerance
The permitted manufacturing range for the ring according to the specified gauge class or engineering requirement.
Calibrated Value
The measured value assigned to that individual ring during calibration.
A ring may therefore:
- Have a nominal size of 25.000 mm
- Meet the required gauge tolerance
- Have a calibrated value that is slightly different from exactly 25.000 mm
Passing its tolerance specification does not mean the ring has zero deviation from nominal.
This is particularly important for master and setting rings.
What Tolerance Class Did You Actually Order?
The phrase “high precision ring gauge” is not a complete specification.
MISHUTE currently lists ring-gauge tolerance classes including:
- XX
- X
- Y
- Z
- ZZ
with customized requirements also available.
The buyer should therefore confirm:
- Required class
- Nominal size
- Gauge function
- Applicable internal specification or standard
- Calibration requirement
Do not select a tighter class only because it appears more precise.
The correct class depends on what the gauge needs to control.
For example, a high-level master ring used to establish another instrument’s reference point may justify tighter requirements than a production limit ring checking a relatively wide shaft tolerance.
Why Measurement Uncertainty Matters
Suppose a certificate reports:
Actual diameter: 25.0002 mm
That value looks extremely precise.
But how much confidence should you place in the last digit?
That is where measurement uncertainty becomes relevant.
Uncertainty reflects the combined effects of factors such as:
- Reference standard
- Measuring instrument
- Repeatability
- Temperature
- Alignment
- Contact conditions
- Bore geometry
- Measurement procedure
For buyers, the important question is not:
Which supplier prints the smallest uncertainty?
It is:
Is the reported uncertainty appropriate for how I plan to use this ring?
Production Ring
A GO/NO-GO production ring may be evaluated mainly against its gauge limits.
Setting Ring
A master setting ring may become part of the uncertainty chain of every bore measurement made after the instrument is set.
The ring’s calibration uncertainty therefore becomes much more significant.
The more measurement responsibility the ring carries downstream, the more important its calibrated value and uncertainty become.
Do Not Ignore Roundness When Buying a Master Ring
Consider a setting ring that is slightly oval.
At one orientation, the measuring contacts read one value.
Rotate the ring.
The contact relationship changes.
The result may shift.
A good calibration and inspection strategy should therefore consider whether bore geometry is suitable for the intended reference function.
This does not mean every commercial calibration certificate must contain a full roundness trace.
It means buyers should not assume that one diameter number describes every aspect of the internal cylindrical surface.
For demanding master-ring applications, ask whether the supplier controls or verifies:
- Diameter
- Roundness
- Taper
- Cylindrical geometry
- Surface finish
The actual requirement should match the measurement system.
Factory Inspection Report vs Calibration Certificate
This distinction matters during procurement.
MISHUTE states that its ring gauges are inspected before shipment and supplied with calibration/inspection documentation, while third-party certification is also available when required.
But buyers should still specify which level of documentation they need.
| Requirement | Factory Inspection Report | Calibration Certificate |
| Supplier final QC evidence | Strong fit | Yes |
| Confirm gauge manufactured to specification | Yes | Yes |
| Actual assigned master-ring value | May be included | Commonly required |
| Measurement uncertainty | May vary | Important for precision calibration |
| Third-party calibration | No | Can be requested |
| Quality-system traceability | Depends on requirement | Stronger when properly documented |
| Routine production GO/NO-GO use | Often practical | May be unnecessary |
| High-level master/setting use | May not be enough alone | Often more appropriate |
Buy the documentation according to the function of the ring, not simply because one certificate sounds more prestigious.
What Does “Traceable Ring Gauge” Mean for a Buyer?
The word traceable is often treated like a product feature:
Traceable Ring Gauge
From a metrology perspective, that wording is incomplete.
What matters is whether the measurement result can be related through a documented calibration chain to recognized measurement references, with uncertainty accounted for.
For purchasing purposes, look for evidence such as:
- Identified calibration laboratory
- Calibration procedure
- Reference standards
- Measurement result
- Measurement uncertainty
- Certificate identification
- Calibration date
- Applicable traceability statement
If your customer specifically requires third-party or accredited calibration, state that in the RFQ.
MISHUTE indicates that third-party certification can be provided for ring gauges when additional compliance documentation is required.
A Certificate Is More Important for Setting Rings Than Many Buyers Realize
Suppose a technician uses a setting ring to zero a bore gauge.
The measurement chain becomes:
Calibrated Ring → Bore Gauge → Production Bore
An error in the ring’s assigned value can therefore influence every subsequent production measurement.
For this reason, purchasing a master or setting ring solely by nominal size misses part of its function.
When sourcing master setting ring gauges, consider requesting:
- Actual calibrated diameter
- Measurement uncertainty
- Ring identification
- Calibration date
- Relevant calibration documentation
The reference value should then be managed within the company’s measurement-control system.
Does Every GO/NO-GO Ring Need the Same Certificate?
Not necessarily.
Imagine a production line with 20 working ring gauges.
They inspect external diameters every day.
The company also owns two master rings kept in a controlled metrology room.
Treating all 22 rings identically may not be the most efficient calibration strategy.
Working Ring Gauges
Key concerns may include:
- Wear
- Size limit
- Frequent handling
- Production risk
- Verification frequency
Master Rings
Key concerns may include:
- Stable assigned value
- Lower wear
- Controlled storage
- Measurement uncertainty
- Calibration history
- Traceability
A risk-based calibration system may therefore use different verification and documentation levels for different rings.
Material Changes the Calibration Strategy
MISHUTE provides ring gauges in hardened steel, zirconia ceramic, and tungsten carbide.
Material does not remove the need for calibration, but it influences how the gauge behaves in service.
Hardened Steel
Commonly practical for general inspection.
Monitor:
- Wear
- Corrosion
- Handling
- Storage condition
Tungsten Carbide
Often selected for intensive production use where wear resistance is important.
This can be useful for high-cycle ring gauges that repeatedly contact production parts.
Zirconia Ceramic
Useful where corrosion resistance and non-magnetic behavior are important.
This can reduce some environmental maintenance concerns.
A wear-resistant material can help preserve gauge size, but it does not eliminate calibration or periodic verification.
How Often Should a Ring Gauge Be Recalibrated?
There is no single calibration interval that is appropriate for every ring gauge.
A useful interval should reflect:
- Ring function
- Usage frequency
- Material
- Wear history
- Previous calibration results
- Storage conditions
- Inspection risk
- Customer requirements
- Quality-system requirements
A Production Ring May Need More Frequent Monitoring When
- It is used for 100% inspection
- The workpiece material is abrasive
- Operators handle it continuously
- Past calibration shows measurable wear
- Accepting an oversize or undersize component creates high risk
A Master Ring May Justify a Different Interval When
- It is used infrequently
- It remains in a controlled room
- It has stable calibration history
- Intermediate checks indicate stability
The most useful strategy is to review actual calibration history rather than mechanically replacing one date with another every year.
Historical Data Can Reveal Wear Before Failure
Consider this simplified example:
| Calibration Event | Measured Diameter |
| Initial | 25.0001 mm |
| Calibration 2 | 25.0002 mm |
| Calibration 3 | 25.0004 mm |
| Calibration 4 | 25.0007 mm |
The values are illustrative.
What matters is the trend.
For a working ring gauge, repeated dimensional movement may indicate:
- Wear
- Surface damage
- Heavy usage
- Contamination or cleaning issues
- Need for a shorter verification interval
For a master ring, unexpected changes may trigger an investigation into:
- Handling
- Storage
- Calibration method
- Environmental effects
Calibration history therefore turns the certificate from a filing requirement into a maintenance tool.
Seven Details Buyers Should Check Before Accepting the Certificate
Instead of simply filing the PDF, run through these seven questions.
1. Can I Identify the Physical Ring?
Check serial number, gauge ID, size, and type.
2. Is the Gauge Function Clear?
Is it:
- GO
- NO-GO
- Master
- Setting ring
The result should be interpreted according to its role.
3. Is the Actual Size or Deviation Reported Where Needed?
This is particularly important for master and setting applications.
4. Is Measurement Uncertainty Available?
For high-accuracy reference use, this can be critical.
5. Does the Certificate Match the Purchased Tolerance Class?
Do not assume that all “precision rings” are equivalent.
6. Is Traceability Adequately Documented?
Look beyond a marketing statement.
7. Does the Documentation Meet Your Customer Requirement?
A technically valid factory report may still be insufficient if your contract specifically requires third-party calibration.
Common Procurement Mistake: Requesting the Certificate After the Ring Is Finished
This happens frequently:
- Purchasing requests a ring gauge.
- Supplier quotes production only.
- Gauge is manufactured.
- Quality department asks for accredited third-party calibration.
- Additional cost and lead time appear.
The certificate requirement should therefore be written into the original RFQ.
For example:
Plain master setting ring, Ø40 mm, required tolerance class X, tungsten carbide, intended for setting an internal comparator. Individual calibrated diameter and third-party calibration certificate required.
This is much clearer than:
Quote one 40 mm ring gauge with certificate.
A Better Ring Gauge RFQ
A professional request can contain:
| RFQ Item | Example |
| Gauge type | Master setting ring |
| Application | Setting a bore gauge |
| Nominal diameter | Ø40 mm |
| Required class | X |
| Material | Tungsten carbide |
| Actual calibrated value | Required |
| Measurement uncertainty | Required |
| Quantity | 2 pcs |
| Gauge identification | Individual serial number |
| Documentation | Factory report + third-party calibration |
| Usage environment | Controlled QC room |
For a production ring:
| RFQ Item | Example |
| Gauge type | GO plain ring |
| Application | CNC shaft inspection |
| Workpiece limits | According to drawing |
| Ring limit | According to approved gauge design |
| Material | Hardened steel |
| Quantity | 5 pcs |
| Usage | High-frequency production inspection |
| Documentation | Factory inspection report |
| Marking | GO + size + gauge ID |
The documentation is different because the measurement responsibility is different.
Five Red Flags in Ring Gauge Calibration Documentation
Red Flag 1: Only the Nominal Diameter Appears
For a master ring requiring an assigned value, nominal size alone may be insufficient.
Red Flag 2: There Is No Unique Gauge Identification
The certificate cannot reliably follow the physical tool.
Red Flag 3: “Traceable” Appears With No Supporting Information
Ask what establishes traceability of the measurement result.
Red Flag 4: No Uncertainty Is Available for a High-Level Reference Ring
A master ring used in precision calibration should have enough data to support the user’s uncertainty analysis.
Red Flag 5: The Document Does Not Match the Required Calibration Level
A factory report is not automatically equivalent to a requested third-party calibration certificate.
When Purchasing Price Should Not Be Compared Alone
Suppose Supplier Option A includes:
- Ring gauge
- Factory report
Option B includes:
- Ring gauge
- Individual calibrated value
- Uncertainty
- Third-party calibration
The two prices are not directly comparable because the scope is different.
Before comparing quotations, normalize:
- Material
- Tolerance class
- Ring function
- Calibration level
- Certificate type
- Quantity
- Custom marking
- Inspection requirement
For B2B sourcing, documentation can be part of the product specification rather than an optional piece of paper.
Buyers comparing precision ring gauge calibration options should therefore define both mechanical and documentation requirements in the same RFQ.
What to Ask a Ring Gauge Manufacturer
When sourcing production or master rings, verify that the manufacturer can support:
- Appropriate ring gauge tolerance classes
- GO and NO-GO production rings
- Master and setting rings
- Steel, ceramic, and tungsten carbide
- Custom nominal sizes
- Controlled bore geometry
- Individual identification
- Factory dimensional inspection
- Calibration documentation
- Third-party certification when required
MISHUTE currently lists multiple tolerance classes, three primary material options, pre-shipment inspection, and calibration documentation capabilities for its ring gauge manufacturing service.
For wider dimensional inspection requirements, buyers can also work with MISHUTE as a precision gauge manufacturer rather than sourcing each gauge category independently.
Frequently Asked Questions
What does ring gauge calibration check?
Ring gauge calibration verifies the dimensional condition of the gauge bore. Depending on the application, this may include the actual internal diameter, deviation from nominal, and other characteristics required to establish whether the ring remains suitable for production or reference use.
What should a ring gauge calibration certificate include?
A useful certificate should identify the ring, show the nominal size and relevant calibrated result, state the calibration date, and provide measurement uncertainty and traceability information when required by the intended application.
Is a ring gauge inspection report the same as a calibration certificate?
Not necessarily. A factory inspection report normally confirms the manufacturer’s final dimensional inspection. A calibration certificate may provide a more detailed assigned value, uncertainty, and traceability information.
What is a traceable ring gauge?
In practical metrology, traceability applies to the measurement result rather than simply to the physical ring. The calibration result should be supported by a documented chain of measurement references and associated uncertainty.
Does a setting ring need a calibrated actual diameter?
For precision setting work, knowing the actual calibrated internal diameter can be important because the ring establishes the reference point for the measuring instrument.
Does a GO/NO-GO ring gauge need calibration?
Yes. Working ring gauges need periodic verification because wear, handling, contamination, and damage can change the effective gauging dimension.
How often should a ring gauge be calibrated?
The interval should reflect usage, material, wear history, calibration history, storage, measurement risk, and customer requirements. There is no universal interval that is optimal for every ring gauge.
What is the difference between a master ring and a GO ring?
A GO ring directly checks whether an external workpiece passes a dimensional limit. A master ring provides a known reference diameter for setting or verifying another measuring instrument.
Does a carbide ring gauge still need calibration?
Yes. Tungsten carbide provides strong wear resistance, but wear-resistant materials are still precision measuring tools and require verification according to the measurement-control system.
What accuracy should a setting ring have?
The required accuracy should be determined from the measuring instrument being set, the required measurement uncertainty, and the product tolerance. Selecting the tightest available ring class is not automatically necessary.
Can MISHUTE provide ring gauges with calibration reports?
Yes. MISHUTE states that ring gauges are inspected before shipment and supplied with inspection/calibration documentation, with third-party certification options available when required.
Conclusion: Calibrate the Ring According to Its Measurement Responsibility
The important question is not simply:
Does this ring gauge have a certificate?
The better question is:
Does this certificate provide enough information for the way this ring will actually be used?
A production GO/NO-GO ring primarily needs reliable confirmation that its gauging limit remains correct.
A master or setting ring carries greater downstream measurement responsibility and may require:
- Individual calibrated diameter
- Measurement uncertainty
- Stable gauge identification
- Traceability information
- Appropriate third-party calibration
The closer a ring gauge sits to the top of your measurement chain, the more important its calibrated value and supporting certificate become.
Before placing an order, define the ring type, nominal size, tolerance class, material, expected use, required measurement data, and certificate level together.
MISHUTE provides calibrated precision ring gauges for production, master, and setting applications, with multiple tolerance classes, material options, inspection reports, and additional certification options available according to project requirements.